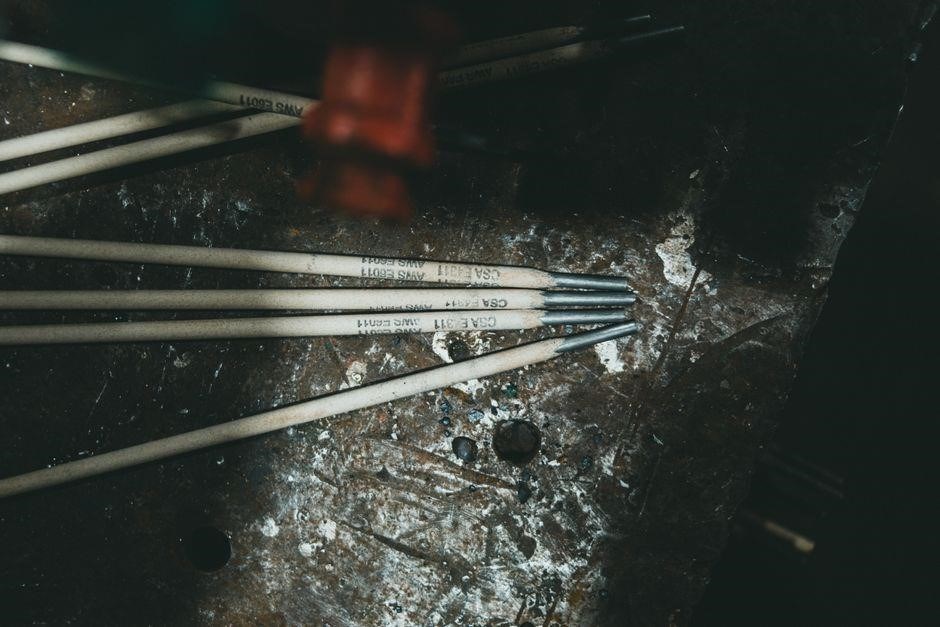
A welding electrode chart PDF offers a concise reference for rod sizes, amperage ranges, and metal thicknesses. It lists common SMAW rods such as 6010/6011 with diameters 3/32″–1/8″, corresponding amperage 40–125 A, and thickness guidelines in inches and millimeters. This tool helps welders select the right electrode for each job.
Types of Welding Processes Covered in Charts
Welding electrode chart PDFs cover major arc methods, primarily Shielded Metal Arc Welding (SMAW) and Gas Metal Arc Welding (GMAW). They list rod types, sizes, and current ranges for each process, allowing welders to match electrode selection with material thickness and joint configuration.
They list rod types, sizes, and current ranges for each process, allowing welders to match electrode selection with material thickness and joint configuration.
Charts aid weld choice.!
Shielded Metal Arc Welding (SMAW) Chart Details
In a typical SMAW chart PDF, each electrode is listed with its designation, diameter, recommended amperage range, and suitable metal thickness. For example, the 6010/6011 rods are available in 3/32″ (2.4 mm) and 1/8″ (3.2 mm) sizes. The 3/32″ rod requires 40–85 A for 1/8–3/16″ (3–8 mm) thick steel, while the 1/8″ rod is used at 75–125 A for 1/4–1/2″ (6–12 mm) thickness. These values are rounded to the nearest whole ampere and are meant for mild steel; stainless or alloy steels may need adjustments.
Other common SMAW electrodes include 6013, 6014, 6015, and 6016. The 6013 rod, a general‑purpose electrode, typically comes in 3/32″ and 1/8″ diameters with amperage ranges of 45–90 A and 70–140 A, respectively. The 6014 and 6015 rods, designed for thicker materials, require 90–150 A for 3/32″ and 120–200 A for 1/8″. The 6016, a high‑strength rod, is usually used at 120–250 A for 1/8″ to 1/4″ diameters. Each chart also indicates the recommended travel speed, shielding gas (if any), and joint type (butt, fillet, or lap)!!
When using a PDF chart, welders should cross‑reference the material type, thickness, and desired weld bead profile. For instance, a 6015 rod on 1/4″ steel at 140 A yields a smooth, low‑porosity bead suitable for structural applications. If the material is thinner than the chart’s minimum, the user should reduce amperage by 10–20 % or switch to a smaller diameter rod. Conversely, for thicker plates, increasing amperage within the chart’s upper limit and using a larger diameter rod will improve penetration.
Some charts also provide a “maximum” amperage for each rod, ensuring the arc does not exceed the electrode’s capacity and cause excessive slag or burn‑through. The PDF format allows quick printing or digital reference on the shop floor, and many manufacturers include a QR code linking to an online version for easy updates. By following these guidelines, welders can achieve consistent, high‑quality welds while staying within safety and performance parameters.
Electrode coatings vary from flux‑core to zinc‑coated, affecting slag removal and bead shape. A zinc‑coated rod, such as 6012, produces a bright, low‑slag bead ideal for outdoor work, whereas a flux‑core rod like 6010 offers better penetration on thicker plates. The chart will specify the recommended polarity—usually DCEN for SMAW—and the optimal travel speed, often 1–2 inches per second for 3/32″ rods and 0.5–1 inches per second for 1/8″ rods. Adjusting travel speed can fine‑tune bead width and penetration depth.
Preheat is rarely required for mild steel in SMAW, but for high‑strength or low‑carbon steels, a preheat of 200–300 °F can prevent cracking. Post‑heat may be necessary for thicker plates to relieve residual stresses. The chart may list recommended preheat temperatures, but these are usually found in material‑specific guidelines rather than the electrode chart itself.
Maintaining the electrode holder and ensuring a clean tip are essential for reliable arc stability. A worn tip can cause arc flicker, leading to inconsistent welds. The chart’s PDF often includes a quick reference table for tip wear limits, such as 0.015″ for 3/32″ rods and 0.020″ for 1/8″ rods. Replacing the tip before exceeding these limits preserves weld quality and extends electrode life.
Proper storage of electrodes—sealed in a dry environment—prevents moisture absorption, which can degrade the flux coating and cause excessive spatter. The chart PDF may include a storage recommendation, such as keeping rods in a sealed bag with desiccant packs. Moisture‑laden electrodes can produce weak arcs and increased slag, compromising weld integrity.
Ambient temperature and humidity influence electrode performance. In cold conditions, the arc may become unstable, requiring a slight increase in amperage or a switch to a thicker rod. In humid environments, moisture on the workpiece can lead to porosity; pre‑cleaning with a wire brush or using a degreaser before welding mitigates this risk.
Always verify the chart against the manufacturer’s datasheet for the specific electrode batch. Consult the chart before each job to ensure compliance with code requirements. Use the chart as a baseline, not a strict rule. Adjust settings based on real‑time feedback. Remember to keep the electrode tip clean. Check for slag buildup after each weld. Always follow safety gear. Always follow safety gear guidelines.
Gas Metal Arc Welding (GMAW) Chart Details
In a GMAW chart PDF, wire size, amperage, thickness, gas, and travel speed are listed. A 0.035″ (0.9 mm) wire runs 70–120 A for 1/8–1/4″ steel, while a 0.045″ (1.1 mm) wire uses 120–200 A for 1/4–1/2″ material. Gas is 75 % Ar/25 % CO₂ for mild steel, 100 % CO₂ for alloys, and 100 % Ar for stainless. Flow rates are 20–30 cfm. The chart also lists the recommended wire feed speed to match amperage and prevent overheating.
Travel speed is 1.5–2.5 in/s for 0.035″ wire and 1–1.5 in/s for 0.045″ wire to achieve a smooth bead. The chart also specifies acceptable workpiece temperatures (200–400 °F for high‑strength steel) and recommended preheat for thin sections (≈200 °F for 1/8″ plates). It also specifies the recommended travel speed range for bead width control.
Wire preparation is critical. Clean the wire with a brush or cleaner before feeding to remove oil, rust, or paint. Keep the spool level and rotate it consistently to avoid tangles. The chart specifies a feed speed of 200–400 in/min for 0.035″ wire and 400–600 in/min for 0.045″ wire. The chart indicates max wire feed speed to avoid excessive heat input.
Ambient conditions affect gas flow and arc stability. In cold weather, increase gas flow or amperage to counter condensation. In humid air, pre‑clean the surface to reduce spatter. The chart recommends a pre‑heat blanket for thin sections to prevent cracking and maintain bead integrity. It also suggests using a lower amperage for very thin plates to avoid burn‑through.
Many charts reference welding codes like AWS D1.1 for structural steel or AWS A5.1 for stainless. They show minimum penetration for each thickness, ensuring code compliance. Adjust settings based on the chart and verify against the specific code section. If the chart indicates a minimum of 0.5× thickness, the weld must penetrate at least that amount. Always cross‑check with the latest manufacturer data sheet and adjust settings if necessary. Follow the chart for optimal results. It also lists recommended arc voltage ranges to aid machine setup!!!
Common Electrode Size Ranges and Measurements
Typical SMAW rods span 3/32″ to 1/4″ (2.4–6.4 A). 6010/6011 rods are 3/32″ (40–85 A) or 1/8″ (75–125 A). Wire diameters convert: 3/32″≈2.4 mm, 1/8″≈3.2 mm, 1/4″≈6.4 mm. These ranges guide amperage and thickness selection for reliable welds. The chart lists amperage ranges for each diameter, ensuring fusion without burn‑through.
Electrode Diameter Standards (mm and inches)
Electrode diameter is the most fundamental measurement in a welding electrode chart PDF. It determines the current range, penetration depth, and the amount of filler material delivered per unit length; The industry standard for stick welding rods is expressed in both inches and millimeters to accommodate users worldwide. The most common sizes are 3/32″, 1/8″, 1/4″, 5/32″, and 1/2″, which correspond to 2.4 mm, 3.2 mm, 6.4 mm, 4.0 mm, and 12.7 mm respectively. A 3/32″ rod (2.4 mm) is ideal for thin sheet metal and light structural work, requiring 40–85 A. A 1/8″ rod (3.2 mm) is versatile, suitable for medium‑thickness plates and structural welds, with a typical range of 75–125 A. A 1/4″ rod (6.4 mm) delivers high penetration and is used for heavy‑section steel, often operating between 120–170 A. The 5/32″ rod (4.0 mm) fills the gap between 1/8″ and 1/4″, providing 90–140 A for medium‑to‑heavy work. A 1/2″ rod (12.7 mm) is reserved for the thickest plates and structural members, where 200–300 A may be necessary. When converting inches to millimeters, remember that 1″ equals 25.4 mm, so 3/32″ equals 2.4 mm (3 × 0.8 mm). Accurate diameter selection ensures proper arc stability, reduces distortion, and improves weld quality. In a PDF chart, these values are typically listed in a table format, allowing quick reference for the welder on the job site. The chart may also indicate the recommended amperage per inch of thickness, the filler metal composition, and the welding position (flat, horizontal, vertical, overhead). By mastering the diameter standards, welders can confidently choose the correct rod, maintain consistent weld bead geometry, and achieve the desired mechanical properties in the finished joint. Additionally, the chart often includes tolerance ranges for diameter, such as ±0.005″, to account for manufacturing variations. Welders should verify the actual rod diameter before use, as a slight deviation can affect the arc current and weld pool dynamics. The standard sizes also align with the American Welding Society (AWS) electrode designations, where the first digit indicates the rod diameter in eighths of an inch. For example, a 6011 rod with a 1/8″ diameter is designated as 6011‑1/8. Understanding this nomenclature helps in quickly locating the correct electrode in the PDF. When reading the chart, pay attention to the units column; some PDFs list diameters in millimeters only, while others provide both units side by side. This dual‑unit presentation aids international welders and ensures no misinterpretation during field work. Thus, a comprehensive electrode diameter standard section in a PDF chart is essential for efficient, safe, and high‑quality welding operations.
Amperage Guidelines for Various Metal Thicknesses
Use these ranges as a baseline; for thicker plates, increase amperage by 10 % per inch beyond the chart’s upper limit. Monitor bead profile to avoid burn‑through and ensure proper penetration. Check the manufacturer’s data sheet for electrode specs and verify rod diameter to ensure quality.Verify rod diameter for use
Thick vs Thin Material Recommendations
When selecting electrodes from a PDF chart, thickness dictates both amperage and rod choice. For thin sheets (≤0.1 in / 2.5 mm), use low‑current rods (e.g., 6011 at 40–70 A) to prevent burn‑through. Thin materials also benefit from finer rods (3/32″–1/8″) that offer better control and reduced slag.
For medium thicknesses (0.1–0.3 in / 2.5–7.5 mm), moderate currents (70–120 A) and medium‑diameter rods (1/8″–1/4″) provide sufficient penetration while limiting distortion. Thick plates (>0.3 in / 7.5 mm) require higher amperage (120–200 A) and larger rods (1/4″–5/16″). Pre‑heat the metal to 300–400 °F (150–200 °C) to reduce cracking risk.
Always match the electrode’s coating to the material: flux‑core for mild steel, E6013 for stainless, E7018 for high‑strength alloys. Adjust travel speed; slower for thick sections to allow heat buildup, faster for thin sections to avoid overheating. Follow the chart’s ranges, but adjust based on joint design, filler size, and welding angle.
For thin materials, use a 6013 rod at 30–50 A for a smooth bead and minimal porosity. For thick sections, a 7018 rod at 150–180 A provides deep penetration and a strong weld pool. With aluminum, use an E4047 rod at 70–100 A for thin sheets, and an E4047‑B at 120–150 A for thicker plates.
Consistent technique, proper foot‑pedal control, and correct electrode angle (10–15°) are essential for quality welds. Wear appropriate PPE, keep the work area well‑ventilated, and verify electrode length matches joint length to avoid excessive sag or under‑penetration.
When working with fillet joints, the filler size should be one diameter smaller than the base material to avoid excessive heat input. For butt joints, use a filler rod that matches the base metal’s grade and thickness to ensure uniform fusion. Pre‑heat thin sections to 200 °F (93 °C) when welding with 6013 to reduce cracking, and post‑heat thick plates to 400 °F (204 °C) for high‑strength alloys to relieve residual stresses.
Remember that the PDF chart often lists a safety margin; stay within the lower bound for thin work to preserve edge integrity, and within the upper bound for thick work to avoid under‑penetration. If the chart shows 80–120 A for a 1/4″ rod on 0.2 in material, choose 90 A for a clean bead and 110 A for deeper penetration.
Reading and Interpreting PDF Electrode Charts
A PDF electrode chart is a compact reference that lists rod diameters, current ranges, and suitable metal thicknesses. The first column typically shows the electrode code (e;g., 6011, 6013, 7018), followed by the diameter in inches or millimeters. The next column lists the recommended amperage range for that rod, while the final column specifies the thickness of metal that the rod can effectively weld.
When you open the chart, locate the section that matches your base material: mild steel, stainless steel, aluminum, or high‑strength alloy. Each material group will have its own set of rods and current limits. Pay attention to the “Amperage” column; it is usually expressed as a range (e.g., 40–70 A). The lower end of the range is suitable for thin work or when you need a finer bead, whereas the upper end is for thicker plates or deeper penetration.
The “Thickness” column is often split into two units: inches and millimeters. This dual listing helps you quickly match the chart to the measurement system you use on the shop floor. For example, a 1/8″ rod may be listed as 3.2 A for 0.1–0.3 in (2.5–7.5 mm) of steel. If your material is 4 mm thick, you would look for a rod that lists 4 mm in its thickness range.
Many charts include a “Coating” or “Flux” designation that indicates the type of slag or shielding gas the rod produces. E6011 rods produce a white slag and are good for outdoor work; E6013 rods produce a gray slag and are ideal for indoor use. E7018 rods have a low‑hydrogen coating, which reduces porosity in critical welds.
To interpret the chart accurately, cross‑reference the rod diameter with the amperage range and the metal thickness. If the chart shows a 1/4″ rod with 120–160 A for 0.3–0.5 in steel, you know that using 140 A will give you a balanced bead. If you exceed the upper limit, the weld may become too hot, causing burn‑through or excessive slag. If you stay below the lower limit, the weld may lack penetration.
Some charts also provide a “Tip” section that offers practical advice: keep the electrode at a 10–15° angle, maintain a steady travel speed, and use a foot‑pedal to control amperage. These tips help you translate the static numbers on the chart into dynamic welding practice.
Finally, remember that a PDF chart is a guideline, not a hard rule. Always test a bead on scrap material before committing to a final weld, especially when working with unfamiliar alloys or thicknesses. Adjust the amperage in small increments until you achieve the desired penetration and bead profile.
Safety Considerations When Using Electrode Charts
Before selecting a rod from a welding electrode chart PDF, ensure all safety protocols are in place. The chart provides technical data, but the welding environment can still pose risks if precautions are ignored.
- PPE: Wear a helmet with the correct shade, flame‑resistant gloves, jacket, and steel‑toe boots. Protect your eyes from UV and infrared radiation.
- Ventilation: Use local exhaust or a fume extractor, especially when working with E6011 rods that produce fine particulates.
- Fire Safety: Keep flammable materials at least 10 ft away. Higher amperage increases heat input, so work on a clean, oil‑free surface.
- Grounding: Secure the clamp to a clean metal surface. Loose connections can arc or shock; stay within the chart’s amperage limits.
- Electrode Handling: Store rods dry, inspect for cracks. A compromised rod can cause inconsistent arcs and blow‑off.
- Arc Length & Angle: Maintain a 10–15° angle and proper arc length to reduce slag spatter and accidental contact.
Arc flash hazard: The chart’s amperage can affect arc flash energy. Use arc flash PPE if the calculated boundary exceeds the worker’s distance. Follow ANSI/ISEA 381‑2014 for protective clothing.
Equipment inspection: Verify the machine’s power supply, no frayed cables, and correct settings before starting. Ensure the ground clamp is tight and the machine is on a stable surface.
Integrating these safety steps with the chart’s technical data ensures quality welds and a protected work environment.
Always cross‑reference the chart’s!! data with the workpiece thickness and material type. Deviations can lead to under‑penetration or excess slag, compromising weld integrity and safety!!
Sources for High-Quality PDF Charts
Finding reliable PDF charts is essential for accurate welding practice. The most trusted sources come from established manufacturers, industry associations, and academic institutions. Below is a curated list of places where you can download up‑to‑date, machine‑specific electrode charts in PDF format.
- Manufacturer Websites: Companies such as Miller, ESAB, Lincoln Electric, and ESAB provide downloadable PDFs for each rod series. These charts include amperage ranges, recommended thicknesses, and safety notes directly from the product data sheet.
- National Institute for Occupational Safety and Health (NIOSH): NIOSH publishes welding safety guidelines and sometimes includes electrode specifications for research purposes.
- American Welding Society (AWS): AWS offers a comprehensive library of welding procedure specifications (WPS) and electrode data. Members can access high‑resolution PDFs through the AWS Digital Library.
- ISO and ASTM Standards: International standards such as ISO 15614 and ASTM A653 contain electrode classification tables. PDFs are available through ISO or ASTM sites, often requiring a small fee.
- University Engineering Departments: Many universities host welding labs and publish course materials. PDFs of electrode charts are often free.
- Online Welding Communities: Forums like WeldingWeb host user‑generated PDFs. Verify data against manufacturer specs before use.
- Government Agencies: The U.S. Department of Energy and EU ECHA provide regulatory documents that sometimes include electrode performance data in PDF;
When downloading, ensure the file is from a trusted source to avoid outdated or wrong data. Always cross‑check the chart’s amperage and thickness ranges with the material you intend to weld. A reliable PDF chart not only saves time but also enhances safety and weld quality. and safety!
Frequently Asked Questions About Welding Electrode PDFs
These FAQs cover common questions about PDF electrode charts, from how to verify accuracy to best practices for using and updating them. Each answer is concise yet practical.
- What is a PDF electrode chart? A digital list of rod sizes, amperage ranges, and thickness guidelines.
- How do I confirm the chart is up‑to‑date? Check the publication date and cross‑reference with the manufacturer’s latest sheet.
- Can I use one chart for all processes? No. Charts are process‑specific; using the wrong one can cause improper settings.
- What safety notes appear? Look for arc‑flash warnings, PPE, and ventilation requirements.
- How match amperage? Align chart’s range with your machine’s output; pick a rod within overlap.
- Regional standard differences? Yes. ISO, ASTM, AWS may vary; verify the standard used.
- Annotate PDF? Yes. Use editors to highlight, note, embed images.
- Corrupted PDF? Download fresh copy or contact support.
- Update charts? Refresh when new rod series released or data sheet updated.
- Free charts? Manufacturer sites, AWS Digital Library, ISO/ASTM portals, universities.
- Share PDF? Yes, if copyright allows redistribution for education.
- Custom rod chart? Contact manufacturer for a custom data sheet.
Using these guidelines ensures you select the correct electrode, set the proper amperage, and maintain safety on every weld. Use them wisely. Again